Building a brighter future for all.
Globenet Green is an Australian owned company. We supply efficient and cost effective technologies and products to help governments and businesses in the medical, education, defence, construction and hospitality segments minimise their carbon footprint.
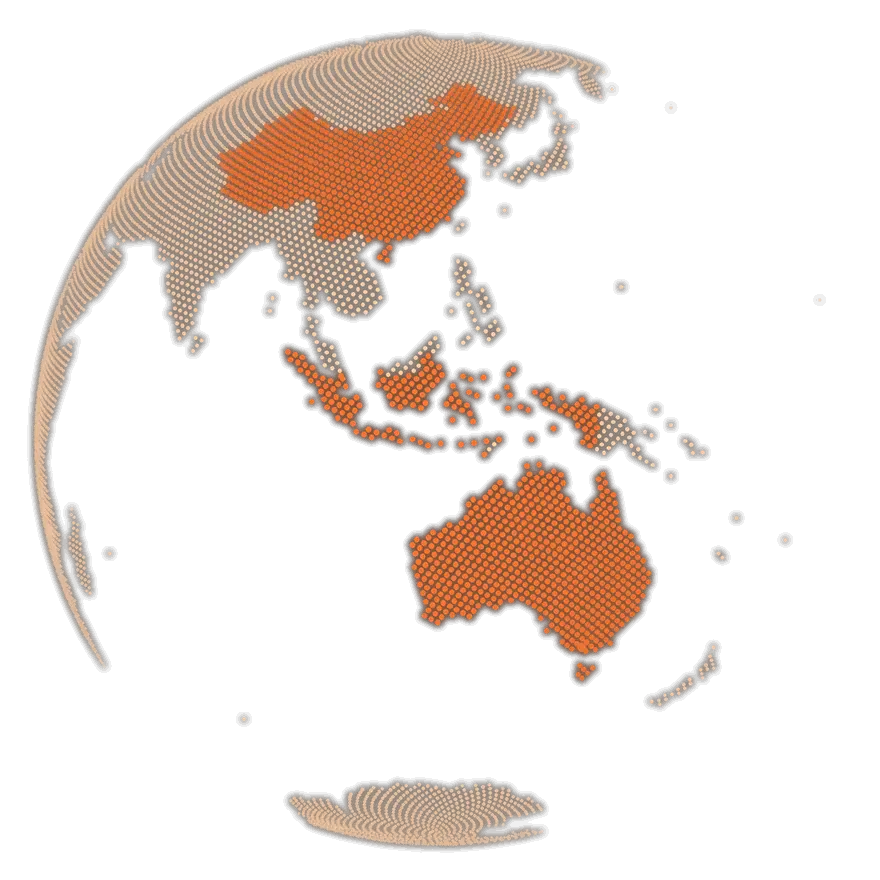
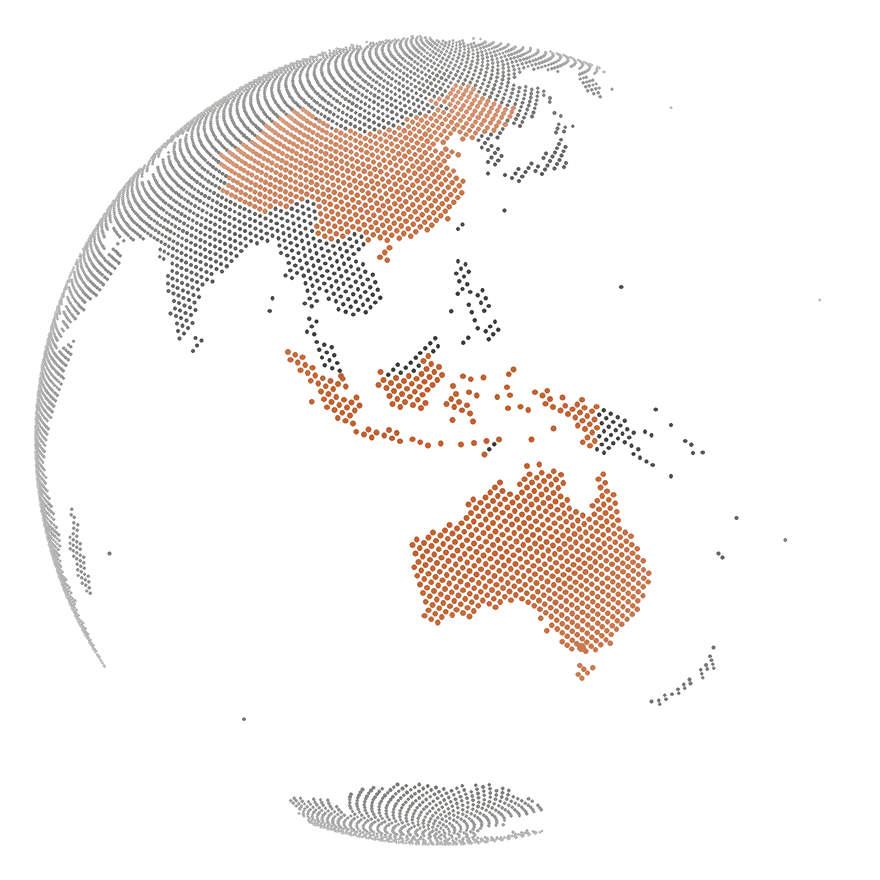
Orange marks our presence in Australia, China, Indonesia and Singapore. Paint it green with your pointer, and drag to spin it.
Light controls
Foreword
- Founded
- 2012
- Australian owned
- AUS
- Headquarters in Melbourne
- MEL
- Countries with a strategic presence
- 4
From our inception as a business, care for people and the planet have been our greatest priorities. We see technology not as an end in itself, but as a tool that can be used to build a brighter future for all. Our goal is to invest in technologies that will help improve lives in the present while building a better and more sustainable world for generations to come.
Following careful consideration of this goal, we have chosen to utilise light-emitting diode (LED) technology, which, thanks to its particular properties, has the capacity to play an important part in addressing many of the environmental, economic and social issues that affect our modern world.
Our focus in both manufacture and development thus far has been lighting. Our ongoing investments into development of other uses of LED technology will allow us to expand beyond lighting, focusing on areas such as health, food production, communications and the Internet of Things. We believe that the use of LEDs in these areas will grow exponentially over time, and will revolutionise our lives. We endeavour to be leaders in technological development in these fields, placing our vision of care and sustainability at the centre of all that we do. We hope that others will share our vision and follow in our footsteps.
Igor KarlikManaging Director
Our goals
- Invest
- Diversify
- Grow
- Stabilise
Lighting for professional customers
Globenet Green supplies sustainable and energy efficient lighting solutions and products to professional customers. All our products are RoHS compliant and environmentally friendly.
Our products use the latest technologies and components from leading brands only, which lets us offer longer warranty periods than most of our competitors. Our engineers are trained by leading experts in the field, and their years of experience help them offer the best solution for each application.
Our strategic presence in Australia, China, Indonesia and Singapore, and our partners around the world, let us find, source and bring to customers the environmentally friendly solutions that suit them best, at the right price. Our network of partners brings expertise not only in manufacturing, design, sales, marketing and logistics, but also in the latest technology, environmental awareness, recycling and energy management.
Leading brands
- Osram
- Bridgelux
- Cree
- Samsung
- Epistar
Segments we serve
- Medical
- Education
- Defence
- Construction
- Hospitality
Designed for specific requirements
Our custom products are designed with specific requirements in mind, and are used in important areas such as emergency lighting, tunnel lighting, hospital surgery rooms, defence applications and mining. Flick a switch to light each one, drag to look around, and paint it green with your pointer.
Emergency lighting
Tunnel lighting
Hospital surgery rooms
Defence
Mining
Tested before it ships
All our products go through a rigorous testing process, and are sold only once they hold the certifications required for their market.
CE, TÜV, SAA and UL are just some of the certifications our products carry. Products meeting specific requirements, such as IP65, can be offered if required.
Our technical expertise includes photometric labs, test material and lighting design.
- CE
- TÜV
- SAA
- UL
- RoHS
- IP65
Our competitive advantages
Technical expertise
Photometric labs, test material and lighting design.
Leading brands
Osram, Bridgelux, Cree, Samsung and Epistar.
Special solutions
Unique luminaires, custom retrofits and system control.
Customer partnerships
Photometric labs, test material and luminaire design.
Global coverage
Branch offices and partners in strategic locations, and certification from various countries.
Established production capability
Factory facilities around the world.
Custom designs
Products can be manufactured to your specifications and requirements.
Promoting quality
Tight quality control ensures high quality products.
Energy saving
LED luminaires need up to 80% less power to produce the same light.
A strong partnership with our customers, an engineering sales force, a focus on providing solutions and up to date manufacturing facilities let us offer what most of our competitors cannot: a long term, sustainable and profitable partnership.